01
Problem
This example explores a manual assembly process that could benefit from consistent sequencing and monitoring of process conditions.
02
Solution
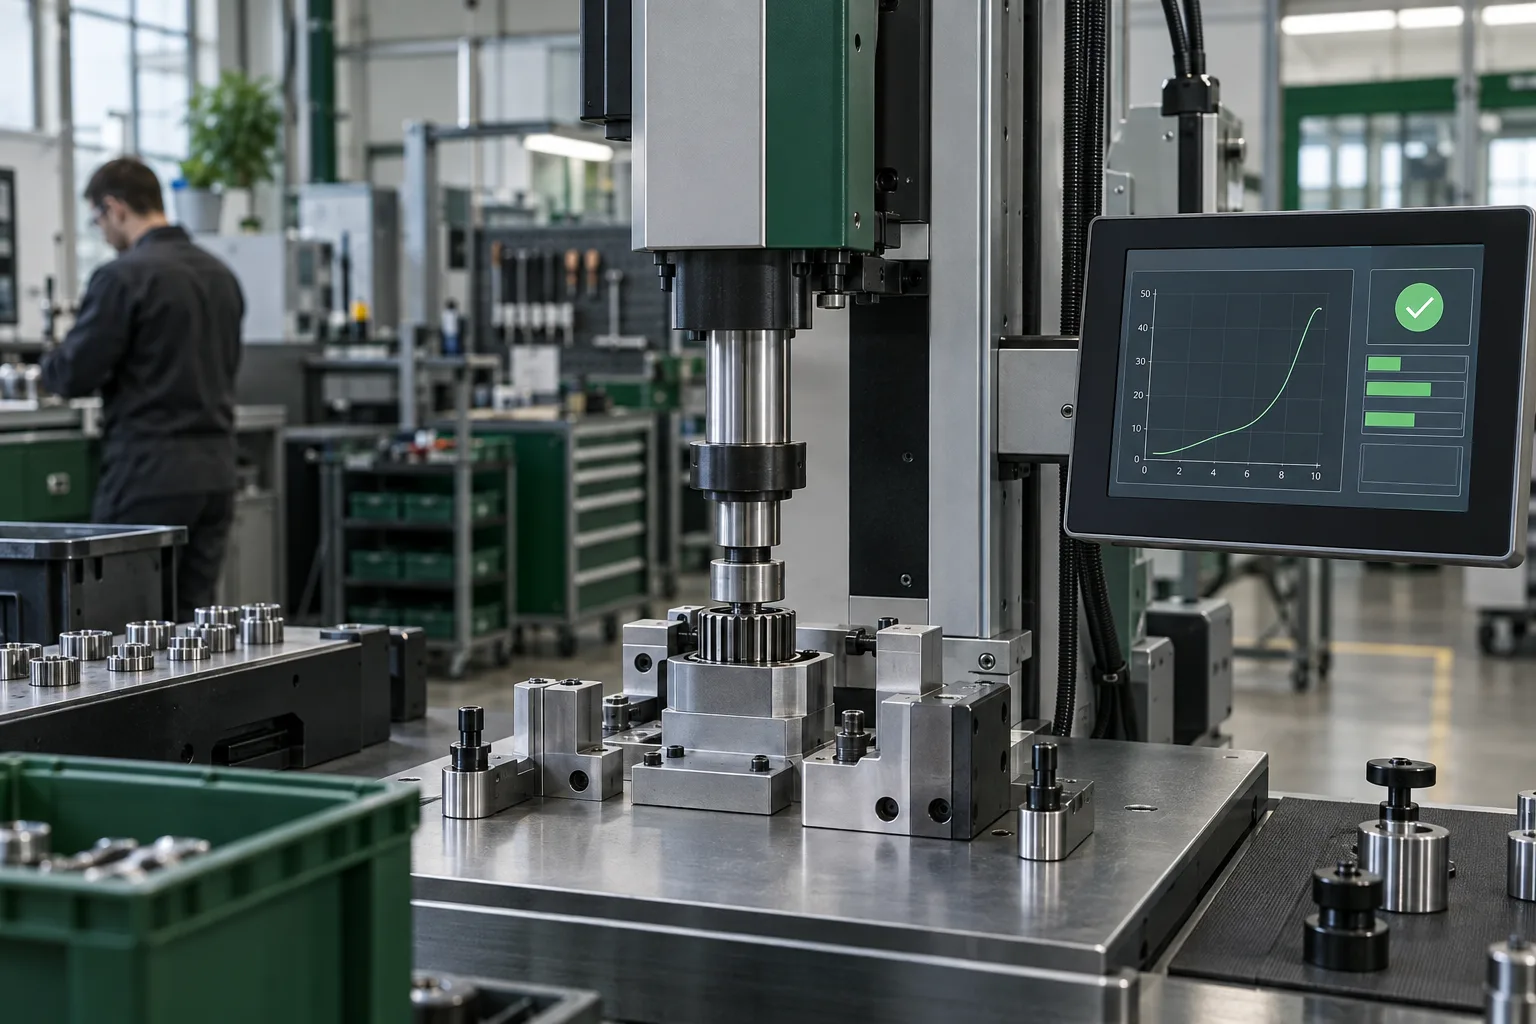
A dedicated fixture, controlled motion axis, part verification sensors and operator interface can be integrated into one station. PLC logic can prevent a cycle from starting when required conditions are not met.
03
System architecture
Part sensors → PLC sequence → controlled motion axis → operator interface. This illustrates an architecture that would be defined for the part and process.
04
Technologies
05
Result
This is an example application scenario. No measured cycle time, quality improvement or completed Petra project results are claimed.